Postion: Home > Our Case > CNC Machining Services >

 CATEGORIES
CNC turning removes material from a rotating workpiece with controlled cutting tools. It is especially effective for parts based on a central axis, including shafts, sleeves, pins, spacers, collars, threaded fittings and precision inserts.
This guide explains the machining process, common features, design considerations, materials, finishing and inspection information needed for a reliable quotation.
Email PDF and STEP/STP files, material, quantity and critical requirements:
info@hms1688.com Leave Contact & Project DetailsThe inquiry form collects contact and basic project information. It does not accept drawing attachments; please email technical files separately.
The workpiece is held in a chuck, collet or other fixture and rotates around the spindle axis. Cutting tools move along or across the axis to create outside diameters, faces, grooves, tapers, bores and threads. Tailstocks, steady rests or other supports may be used for selected long or slender parts.
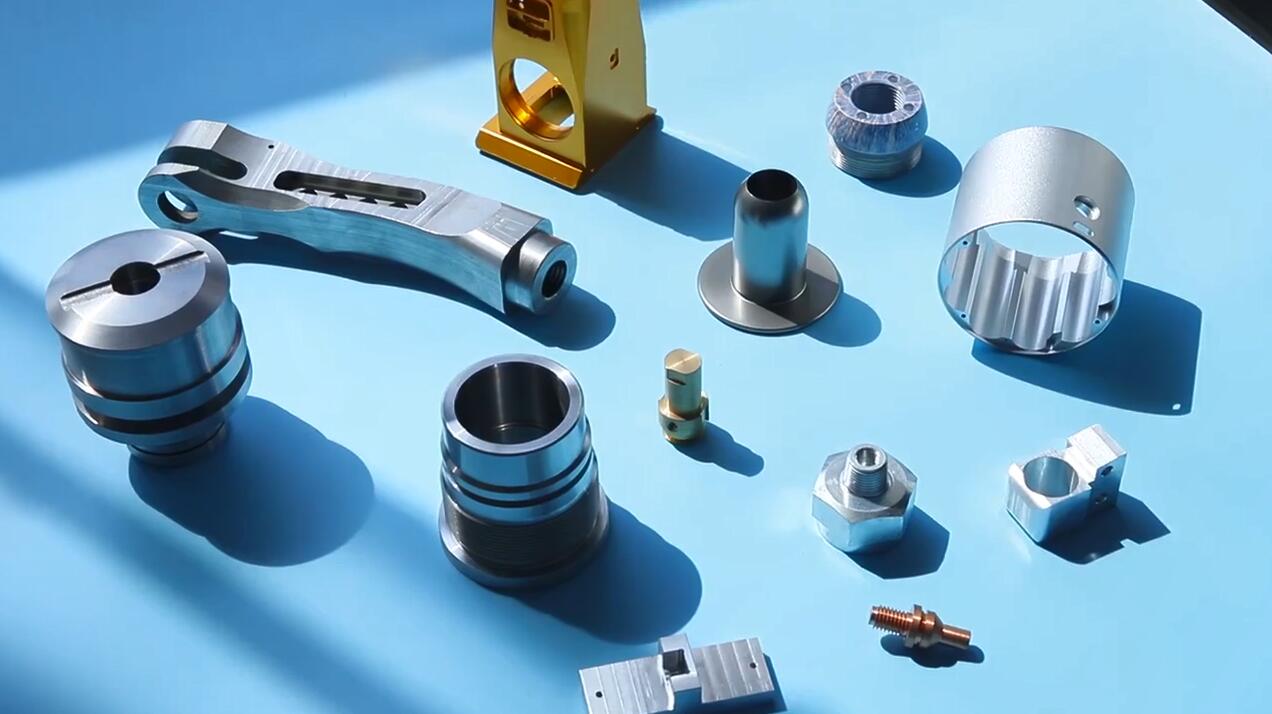 CNC Turning Principle
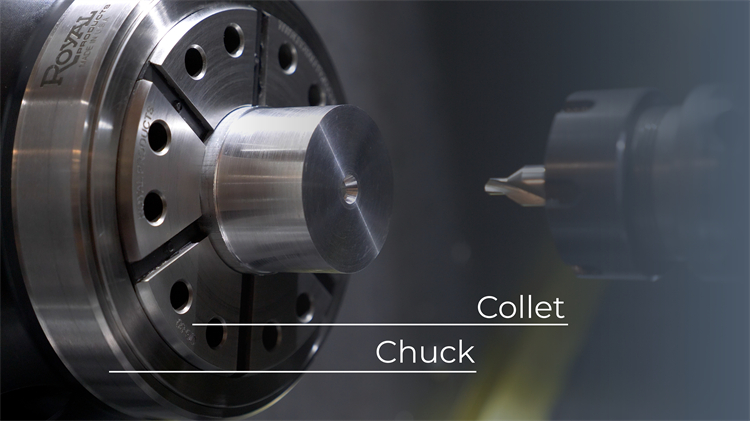 Workholding & Spindle Setup
Outside diameters, faces, shoulders, tapers, chamfers, grooves, external threads and project-dependent knurling.
Drilled holes, bores, reamed diameters, counterbores, internal grooves and internal threads where tool access allows.
Flats, slots, cross holes and off-axis details may require live tooling, turn-mill equipment or a separate milling operation.
Long, slender parts can deflect or vibrate under cutting pressure. There is no single universal ratio limit: material, diameter, unsupported length, tool load, support method and required finish must be reviewed together.
Internal shoulders generally need a radius or relief compatible with the cutting insert and tool access. Larger practical radii often improve tool strength, cycle time and surface consistency.
Small-diameter deep holes are sensitive to chip removal, tool stiffness and coolant access. State depth, diameter, straightness and finish requirements clearly.
Specify width, diameter, corner condition and functional purpose. Standardized geometry can reduce special-tool requirements.
Include standard, size, pitch, class, thread length and any gauge requirement. Provide runout or relief details where assembly depends on full threads near a shoulder.
Apply roughness values only to functional surfaces. Bearing, seal and sliding surfaces may need a specific machining or finishing route.
Mark the functional datum axis and identify concentric, coaxial or runout relationships. Avoid relying on general tolerances for critical rotating interfaces.
 Slender-Part Support Considerations
 OD & ID Turning Tools
| Material Group | Typical Advantages | Machining Considerations |
|---|---|---|
| Aluminum | Low weight, corrosion resistance and good machinability | Alloy, temper, anodizing and cosmetic handling |
| Stainless Steel | Strength and corrosion resistance | Work hardening, heat control, tool wear and passivation |
| Carbon & Alloy Steel | Strength, wear resistance and broad grade selection | Hardness, heat treatment, distortion and corrosion protection |
| Brass & Copper | Conductivity, corrosion resistance and functional appearance | Alloy, burr control, surface condition and plating |
| Engineering Plastics | Electrical insulation, low weight and chemical performance | Thermal movement, stress, moisture and dimensional stability |
| Titanium | High strength-to-weight ratio and corrosion resistance | Heat, tool load, material grade and process review |
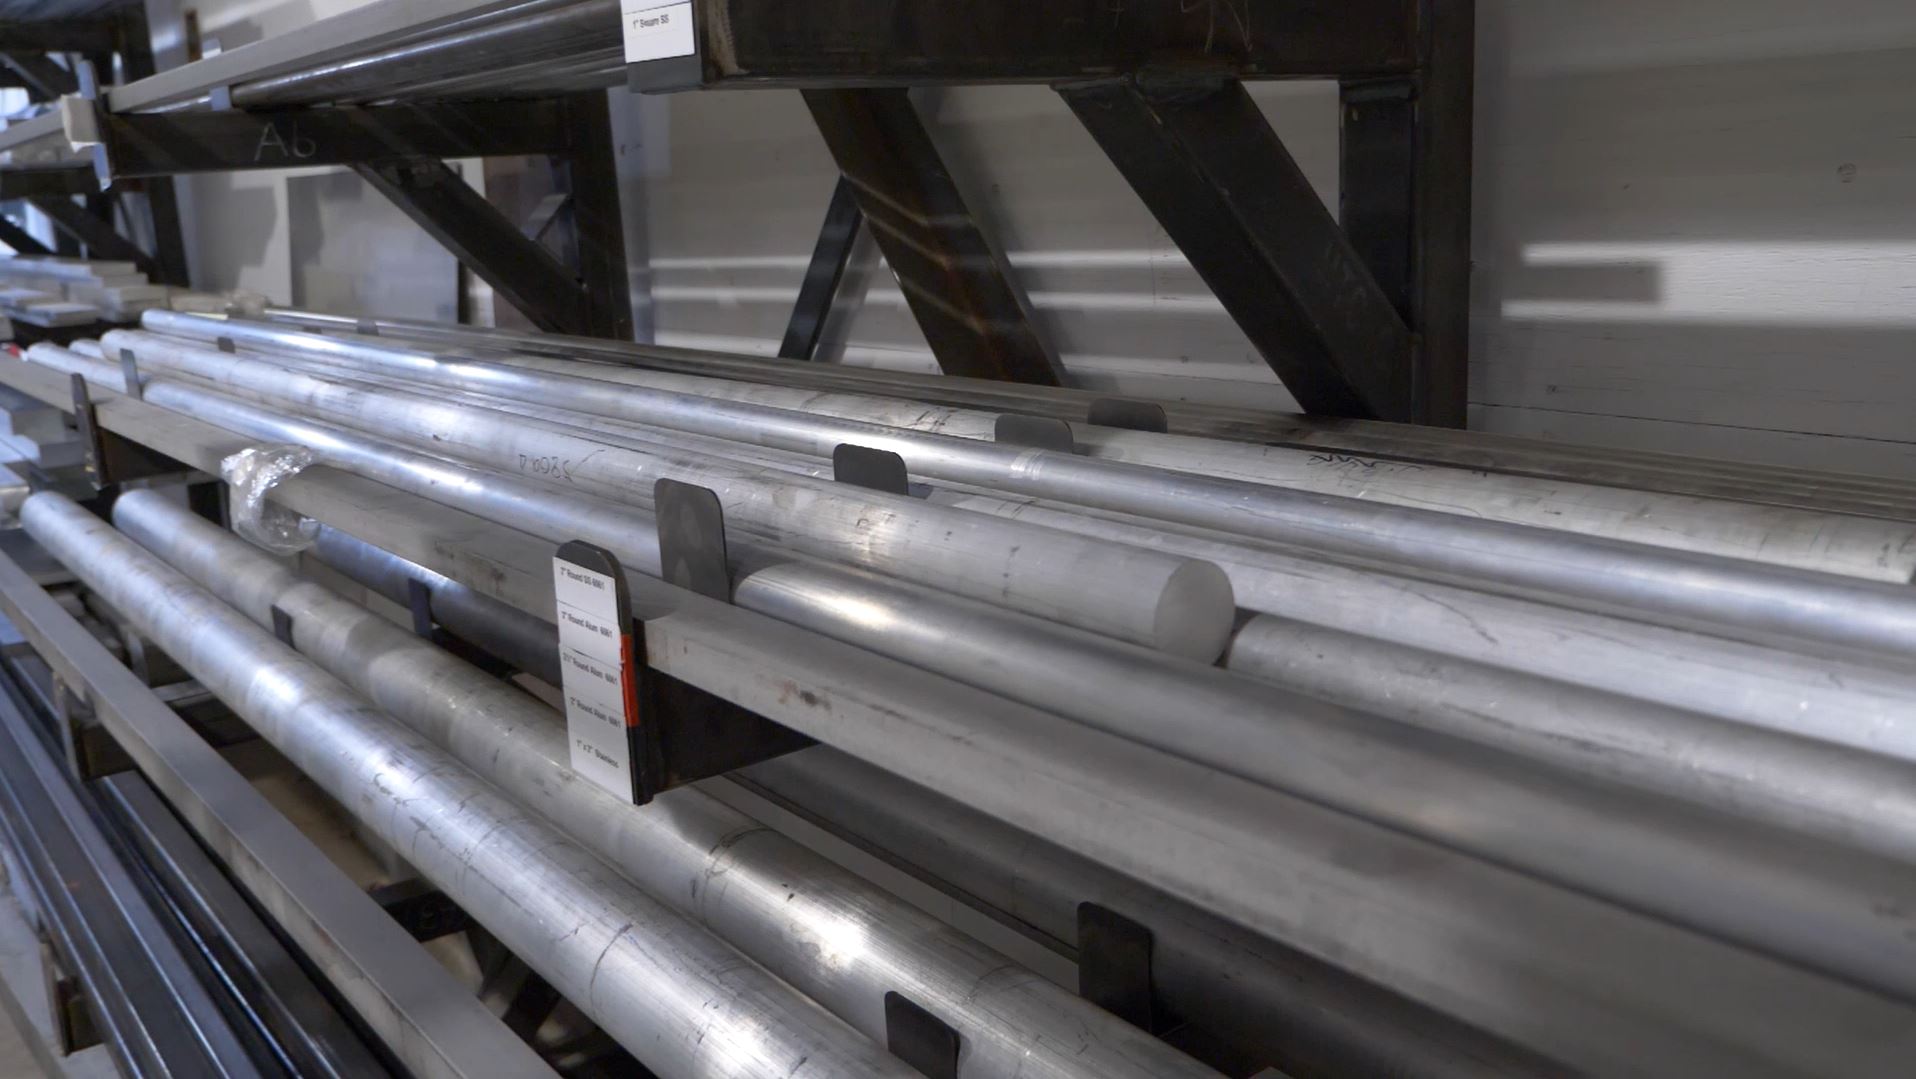 Bar Stock & Material Selection
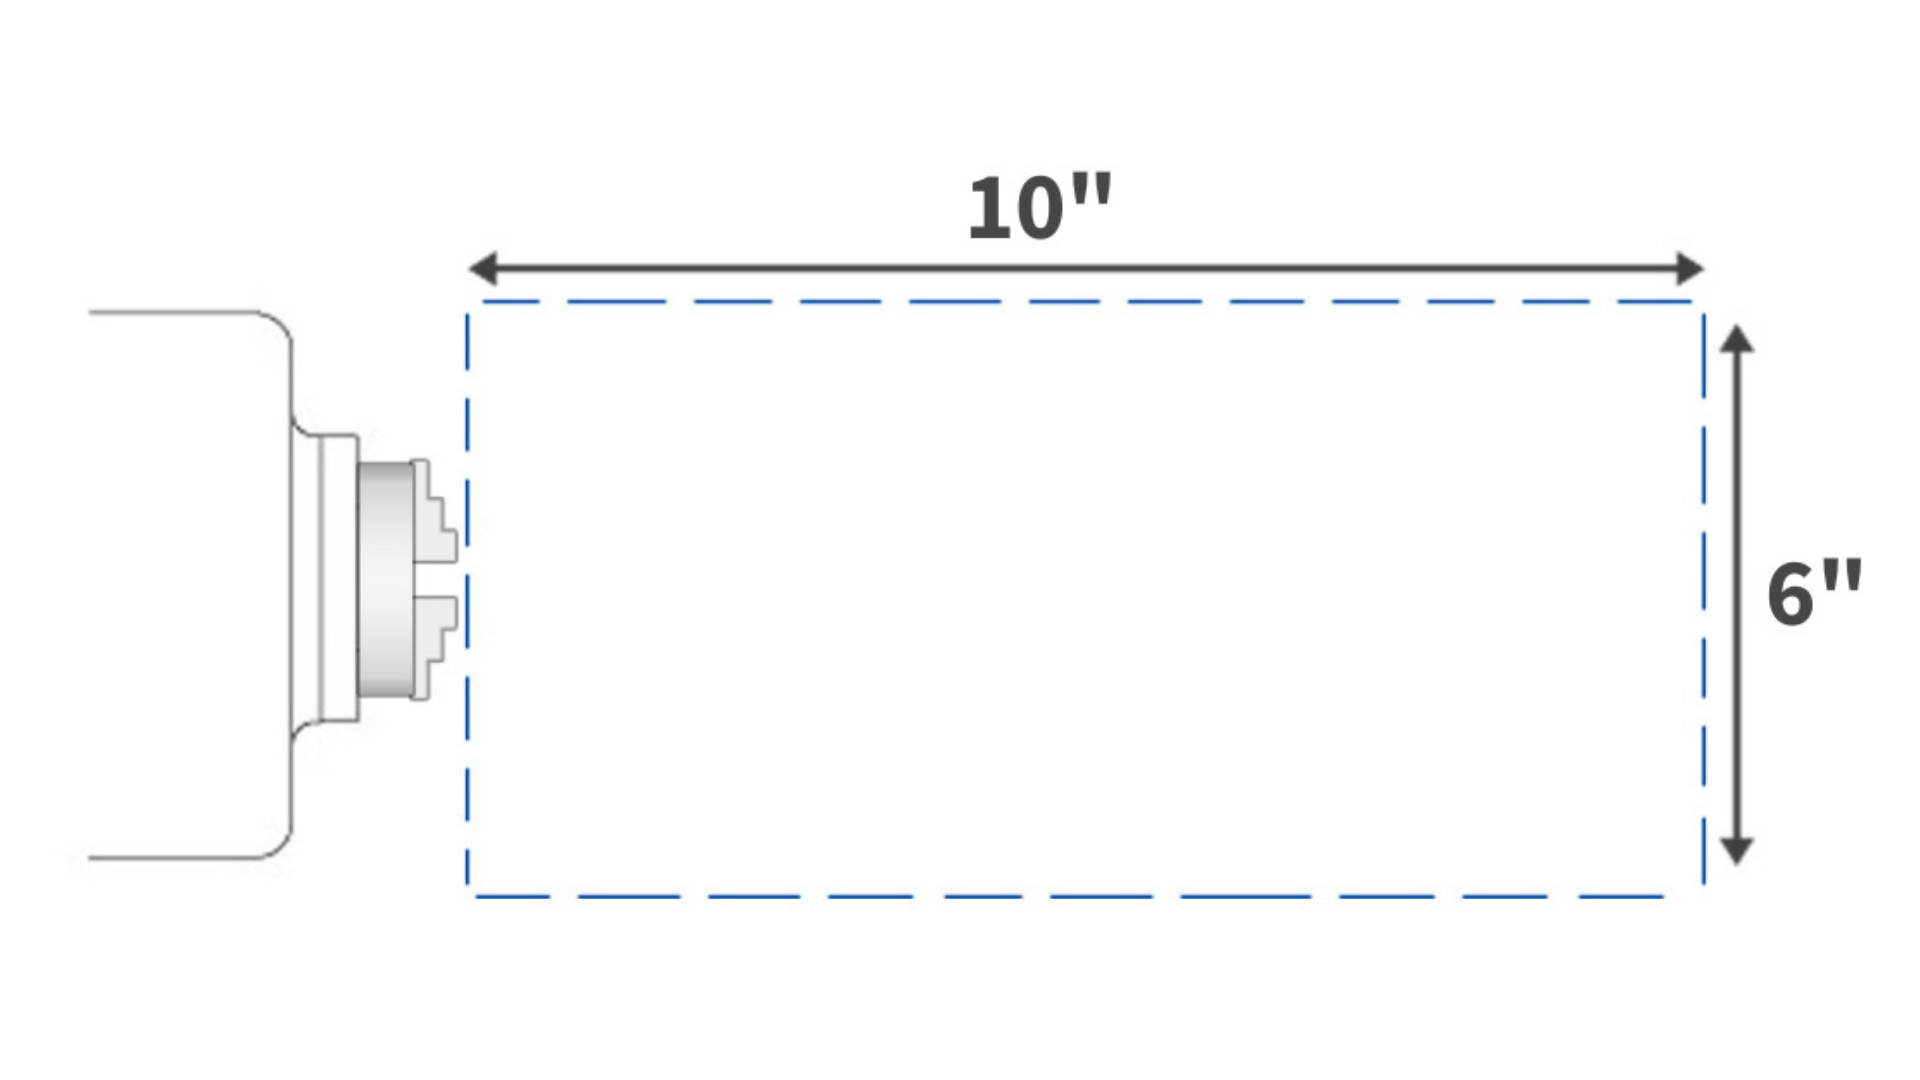 Part Size & Machine Selection
Bar diameter, stock condition, available length, certification requirements and planned finish can affect material sourcing and lead time. Machine capacity should be confirmed for the actual diameter, overall length, through-hole, chucking length and geometry rather than relying on one standard work envelope.
Tool marks remain within the agreed machining standard. It is often suitable for internal or non-cosmetic functional parts.
Deburring, tumbling, bead blasting, brushing or polishing may be used depending on size, geometry and appearance needs.
Anodizing, passivation, plating, black oxide and coating are selected according to material, corrosion, appearance and assembly requirements.
Rotating shafts, pivot pins, locating pins and stepped components for machinery and automation.
Spacers, collars, bearing sleeves, inserts and other close-fitting rotational components.
Threaded fittings, flow-control parts, electrical connectors and custom hardware-type components.
Hongming Sheng manufactures custom CNC turned parts according to drawings, CAD files or approved samples. Send technical files to info@hms1688.com for process and quotation review.
Request CNC Turning ReviewCustomer drawings, models, samples and manufacturing information are handled confidentially. NDA support is available for custom projects.

Contact us and just send us your drawing (SolidWorks,ProE,CAD,PDF,DXF...)
Links: Custom Sheet Metal Enclosure Fabrication | Metal Stamping Services | Sheet Metal Fabrication Services | precision cnc machining and milling services | Metal Welding Services | metal Cutting Services | Metal Bending Service | Metal Surface Treatment & Finishing Solutions |